The manufacturing route behind a carbon fiber plate for shoes decides almost everything a brand later measures on the finished midsole: the stiffness window, batch-to-batch scatter, bond reliability, and landed unit cost. Two plates that look identical in shipping cartons can differ by twenty percen
Introduction
The manufacturing route behind a carbon fiber plate for shoes decides almost everything a brand later measures on the finished midsole: the stiffness window, batch-to-batch scatter, bond reliability, and landed unit cost. Two plates that look identical in shipping cartons can differ by twenty percent in flexural response if the cure cycle drifted or the ply book was wrong, and those differences surface as field returns rather than as lab notes. This article walks the actual production line — sheet lamination, CNC blanking, thermoforming or flat press molding, surface treatment, and inspection — and then hands a sourcing team a concrete set of incoming checks.
We also cover how carbon fiber plates in running shoes programs constrain material choices, which defects sink carbon fiber plate shoes projects at pilot stage, and how tooling amortization and minimum order quantity shape the price stack a factory quotes. The goal is simple: let buyers brief a supplier with the right questions and reject the wrong parts with measured evidence instead of photographs.
Manufacturing Process for a Carbon Fiber Plate for Shoes
Most shoe plates start as flat laminate sheet rather than near-net molded parts. A typical stack is 3K twill or unidirectional prepreg laid in a quasi-isotropic or zero-ninety ply book, cured in an autoclave or under a flat press at 120 to 140 degrees Celsius, then CNC-cut into blanks. Brands that need shaped plates either thermoform the blank over a mold in a short press cycle or compression-mold prepreg directly. The first route is cheaper at low volume because one flat sheet serves several models; the second wins on fiber placement precision once volume justifies dedicated tooling.
- Sheet stage: cure schedule, resin system, and ply book define the stiffness baseline; ask for the cure log, not only the datasheet.
- Blanking: flat-pattern CNC routing keeps fiber continuity; die cutting is faster but frays edges unless tooling is sharp and the sheet is properly supported.
- Forming: thermoforming needs tight temperature control; under-heat leaves springback, overheat degrades the matrix and shows up as surface bloom.
- Finishing: sanding, edge radiusing, and bonding-surface preparation happen after forming and before any top coat or cosmetic film.
Buyer Checks: Incoming Inspection for a Carbon Fiber Plate for Shoe
A buyer receiving plates should not rely on the supplier certificate alone. Pull a sample from each lot and run four checks that take under an hour in any lab: mass against nominal, which catches a wrong ply count within a few percent; a thickness map at five points with a caliper, since flat plates should hold plus or minus zero point one millimeter; a three-point bend spot check on one part per lot, recording deflection at a fixed load and comparing against your own golden sample rather than an absolute modulus; and a visual edge inspection under magnification for voids or delamination. Reject criteria belong in the purchase contract before the first shipment, not in an email after a dispute.
Bonding readiness is the fifth check brands skip most often. Plates that will be glued into a midsole need an abraded, solvent-wiped surface with documented open time; a plate that sat dusty in a warehouse for three months will pass every stiffness check and still fail adhesion. Ask for the surface preparation method and the maximum storage time after treatment, and verify both on incoming lots rather than trusting the first article forever.
What Carbon Fiber Plates in Running Shoes Programs Constrain
Performance running programs impose three constraints that differ from casual footwear. First, the stiffness window is narrow: too stiff and the plate punishes the athlete over marathon distance, too soft and the propulsion benefit disappears; factories must hold that window across lots, which means statistical process control on the press rather than end-of-line inspection alone. Second, mass matters in grams: a five-gram overrun per plate becomes a marketing problem as much as an engineering one. Third, plate geometry interacts with foam, so the same plate in different midsole foams produces different bending behavior and tooling approvals cannot be transferred between foam families without a retest.
Programs at this level also audit traceability. Each lot should carry a roll identifier for the incoming material, a cure batch number, and the press recipe version, because a stiffness shift traced back to a resin roll change is fixable in one phone call while an untraceable shift is only visible after returns climb.
Defects That Sink Carbon Fiber Plate Shoes Projects
Four defects account for most pilot-stage failures. Porosity from inadequate press pressure shows up as scattered low-stiffness readings. Delamination at the trimmed edge usually traces to a dull cutter or the wrong feed rate. Springback after thermoform presents as a rocking plate in the finished shoe, which no consumer photo reveals until wear. Inconsistent bond lines appear when adhesive was applied outside its open-time window. Each defect has a cheap process fix — a revised pressure recipe, scheduled tool maintenance, a tighter form temperature profile, adhesive staging discipline — yet each is invisible in a catalog shot and cheap to catch with the inspection routine above.
| Stage | Common issue | Detection method | Typical cost impact |
|---|---|---|---|
| Sheet cure | Porosity, under-cure | Mass check, thermal analysis on request | 5-15% scrap |
| CNC blanking | Edge fray, wrong outline | Visual under 10x, outline gauge | 2-8% scrap |
| Thermoform | Springback, surface bloom | Flatness map, rocker test | 10-20% rework or scrap |
| Bond prep | Dusty or expired surface | Adhesion pull test per lot | Field failures and returns |
Frequently Asked Questions
What order quantity should a buyer expect for a custom carbon fiber plate for shoes?
Flat plates cut from shared sheet commonly start at 500 to 1,000 pieces per size. Thermoformed plates with dedicated tooling usually need 2,000 to 5,000 pieces before tooling amortizes sensibly. A fully custom outline with a unique ply book should quote tooling separately and typically expects 5,000 pieces or more.
How do factories control stiffness scatter across production lots?
By controlling the variables that drive it — cure cycle, resin batch, ply book — and by running a three-point bend spot check on a fixed schedule. Ask for the control chart and the press recipe version history, not just a pass or fail certificate per shipment.
Can a supplier plate pass inspection but still fail inside the shoe?
Yes, if bonding-surface preparation was neglected or the plate geometry does not match the midsole foam family. Both failure modes require an assembly-level test with the actual foam, not only a plate-level test on the bench.
Conclusion
Treat the plate as a process-controlled commodity rather than a cut-to-shape accessory: audit the sheet stage, run your own incoming checks, and write rejection criteria into the contract before the first lot ships. YongXian laminates and CNC-machines carbon plate for footwear and sporting programs, including quasi-isotropic and zero-ninety stacks, flat and formed outlines, and documented cure and inspection records. Browse carbon sheet and plates or send your plate drawing for a quote.
Part of topic
Related Articles
- Carbon Fiber License Plate: Legality, Durability, and Custom Builds
- Carbon Fiber Rod for RC Plane Builds: Diameters, Joins, and Sizing
- Carbon Fiber License Plate Frame Guide: Materials and Corrosion Notes
- Best Carbon Fiber Plate Basketball Shoes: Court Performance Tradeoffs
- Carbon Fiber Plate for Big Toe: Hallux Rigidus Bracing Options
- Best Carbon Fiber Rod Blanks: Power, Action, and Build Tips
Interested in Our Products?
Contact our team for competitive pricing and technical specifications.
Get a QuoteRelated Products
Round Carbon Fiber Tube — 3K Plain Weave T700
Standard round carbon fiber tube manufactured from Toray T700 grade fiber with 3K plain weave. Offers balanced strength and stiffness for general industrial applications including robotics, automation, sports equipment, and aerospace structures.
Square Carbon Fiber Tube — 3K Twill T700
Square cross-section carbon fiber tube manufactured with 3K twill weave for torsional strength. Preferred for structural frames, trusses, and support columns where rectangular geometry offers design flexibility.
Round Carbon Fiber Tube — UD Unidirectional T700
Unidirectional (UD) round tube with all fibers aligned axially for maximum longitudinal stiffness. Ideal for applications requiring high bending rigidity with minimal weight, such as shafts, struts, and structural reinforcements.
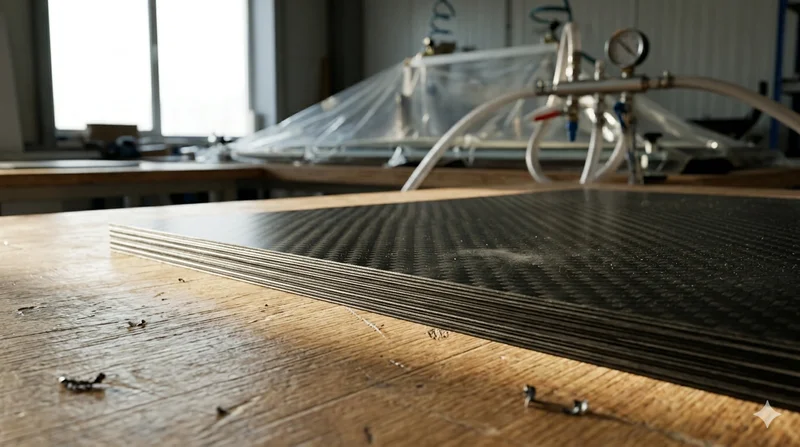
Carbon Fiber Plate — 3K Twill T700 3.0mm
Medium-thickness 3.0mm carbon fiber plate offering significantly higher load capacity while maintaining attractive 3K twill finish. Suitable for structural brackets, reinforcement plates, and load-bearing panels.
Round Carbon Fiber Tube — 3K Twill
Lightweight and ultra-stiff round tubes ideal for drone frames, robotics, and structural applications.