
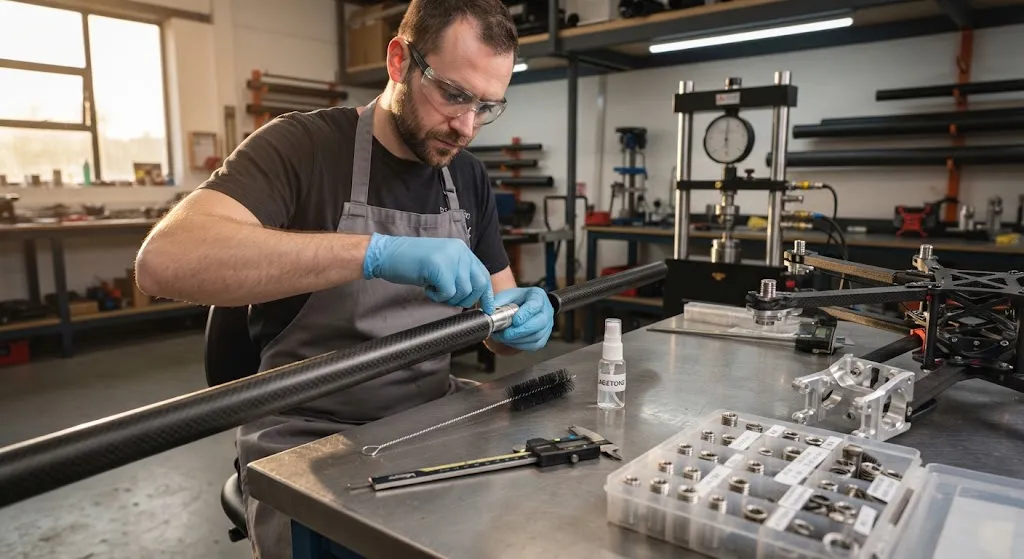
Carbon fiber tube inserts are metal or polymer fittings bonded, pressed, or expanded into the end of a carbon fiber tube so that the tube can be threaded, bolted, or clamped to another component. A pultruded or roll-wrapped carbon tube is a thin hollow shell that cannot be tapped like solid metal, s
Introduction
Carbon fiber tube inserts are metal or polymer fittings bonded, pressed, or expanded into the end of a carbon fiber tube so that the tube can be threaded, bolted, or clamped to another component. A pultruded or roll-wrapped carbon tube is a thin hollow shell that cannot be tapped like solid metal, so the insert is the part that converts the tube end into a real connection point that carries load into a bracket, hinge, or second tube. Every lightweight tripod, drone arm, robot gantry, camera boom, and modular display frame depends on carbon fiber tube inserts to transfer load without crushing the composite wall. Choosing the right insert and installing it correctly is often what separates a frame that stays rigid for years from one that develops a loose, rattling joint after a few assembly cycles.
This guide explains the insert types available, how pull-out strength is actually generated, the installation steps that prevent failure, and the specifications buyers should define when sourcing carbon fiber tube inserts.
What Carbon Fiber Tube Inserts Do
An insert performs four jobs at once, and every design decision should be judged against them:
- Provide a connection point: A threaded insert gives the tube a machine thread, so a bolt, stud, or eyelet can be fastened directly to the tube end.
- Protect the tube end: The composite wall is easily crushed by a bolt head or clamp; the insert spreads that local load over a larger bonded area.
- Distribute load: A bonded or potted insert transfers axial and bending load into the tube wall gradually along its length instead of at a single point.
- Enable assembly and service: Threaded inserts allow components to be assembled, adjusted, replaced, and packed flat without cutting or re-gluing the tube.
Because the tube itself is often stronger than the joint, the insert and its bond are usually the limiting factor in the assembly. Designing for the insert, not just the tube, is the difference between a structure that meets its load case and one that fails at the end fitting.
Types of Carbon Fiber Tube Inserts
Inserts fall into four practical families, each with a different load capacity, installation method, and cost:
- Bonded threaded insert: A machined aluminium or stainless-steel plug with an internal thread is glued into the tube end with structural epoxy. This gives the highest pull-out strength and the widest thread range, but it is permanent.
- Expanding insert: A split sleeve or wedge expands against the tube wall when a bolt is tightened, gripping by friction alone. It needs no adhesive and is removable, but it can ovalise thin tubes and carries less load.
- Rivnut-style sleeve: A tubular threaded sleeve is set into a prepared hole or the tube bore and crimped or bonded in place, giving a low-profile thread with a smaller footprint than a full plug.
- Press-fit polymer insert: A barbed nylon or PA-GF30 insert is pushed into the tube end for light-duty, non-structural joints such as tent poles and display frames.
The table below summarises the typical performance of each type on a 25 mm outside diameter carbon fiber tube with a 1.5 mm wall:
| Insert Type | Typical Pull-Out Load | Thread Range | Removable | Best For |
|---|---|---|---|---|
| Bonded threaded insert | 8-15 kN | M4 to M10 | No | Structural frames, tripod legs, robot arms |
| Expanding insert | 2-5 kN | M5 to M8 | Yes | Adjustable fixtures, field repairs |
| Rivnut-style sleeve | 3-6 kN | M4 to M6 | No | Low-profile panel and bracket fixing |
| Press-fit polymer insert | 0.5-2 kN | M4 to M6 | Partially | Tents, displays, light-duty frames |
The figures assume a correctly prepared bond. A bonded insert installed on an abraded, solvent-wiped surface with a two-part epoxy routinely reaches the top of its range, while the same insert on a mould-release-contaminated surface can lose more than half its capacity.
How Carbon Fiber Tube Inserts Are Installed
Installation quality, not insert cost, controls joint strength. The steps below apply to bonded inserts, which are the most common structural choice:
- Cut and square the tube: Cut with a fine-tooth blade or abrasive wheel, then square and deburr the end so the insert seats fully without a diagonal gap.
- Prepare the bore: Abrade the inner wall with a flapper or bottle brush and wipe it with solvent to remove mould release and dust. This step alone can double bond strength.
- Control the adhesive gap: Aim for 0.05-0.20 mm between the insert and the tube wall. A loose fit relies on a thick adhesive layer that fails in peel; a tight fit starves the joint of adhesive.
- Apply structural adhesive: Use a two-part epoxy rated 20-35 MPa shear strength and apply it to both surfaces with a small rotation to spread it evenly.
- Cure before loading: Hold the assembly straight and undisturbed for the full cure time, typically 24-48 hours at room temperature, or follow the adhesive's heat-cure schedule for faster turnaround.
For expanding and press-fit inserts, the critical controls are bore tolerance and wall thickness. A split-type insert on a tube with a wall below 1.2 mm concentrates stress at the expansion zone and is a common cause of ovalisation, so a bonded insert with a metal liner is the safer choice on thin walls.
Pull-Out Strength: What the Numbers Show
Pull-out strength is governed by three variables: bond area, adhesive quality, and how well the insert matches the tube bore. Bond area scales with insert length and tube circumference, and an embedded length of four to six times the tube diameter is enough for most structural joints; longer inserts add little because the adhesive shear is already spread over a large area.
| Parameter | Typical Value | Design Note |
|---|---|---|
| Adhesive shear strength | 20-35 MPa | Two-part epoxy, structural grade |
| Recommended embedment | 4-6 x tube diameter | Longer adds little strength |
| Adhesive gap | 0.05-0.20 mm | Thin, uniform layer is strongest |
| Service temperature | -40 to +120 °C | Epoxy creeps above 100 °C |
| Thread engagement | 1.5 x bolt diameter | Prevents thread stripping |
A bonded M8 insert in a 25 mm tube with a 4-diameter embedment typically sustains 8-15 kN in direct tension when the bond is correctly made. Bending loads reduce this figure because the load concentrates at the insert edge, and torsion is lower again unless the insert is keyed or pinned. The practical conclusion is that the bond, not the metal, is usually the weakest link, which is why surface preparation deserves more attention than the insert grade.
Common Failure Modes and How to Avoid Them
Most field failures fall into a small number of repeatable categories:
- Peel failure at the tube mouth: A sharp insert shoulder or a poorly seated bond lets the joint peel open under bending. Chamfer the insert and the tube end, and add a small adhesive fillet at the mouth.
- Crushed or ovalised wall: Over-tightened expanding inserts or direct bolt clamping collapse thin tubes. Use a bonded insert or a wider clamp with a liner.
- Galvanic corrosion: Bare aluminium in contact with carbon in wet or salt service corrodes quickly. Anodise the insert or isolate it with a glass-fibre layer.
- Thread stripping: Too little thread engagement or a soft insert alloy strips under load. Specify 1.5 times the bolt diameter in engagement and a 6061-T6 or stainless insert.
- Adhesive starvation: A too-tight fit leaves no adhesive and a dry joint. Check the fit on a scrap section before production.
Sourcing Carbon Fiber Tube Inserts
When buying carbon fiber tube inserts, define the following in writing:
| Specification Item | What to Define | Why It Matters |
|---|---|---|
| Tube outside diameter and wall | Exact OD and wall thickness | Sets insert diameter and bond gap |
| Insert material | 6061-T6 aluminium, 303/304 stainless, brass, or PA-GF30 | Determines strength, weight, corrosion |
| Thread size and pitch | M4, M5, M6, M8 or custom | Must match the mating fastener |
| Insert length | 4-6 x tube diameter embedment | Controls pull-out capacity |
| Finish | Anodised, passivated, or bare | Protects against galvanic corrosion |
| Validation data | Pull-out test certificate | Confirms the joint meets the design load |
Most buyers begin with a search for carbon fiber tube inserts near me or carbon fiber tube inserts suppliers, and many then compare a local machinist with a carbon fiber tube inserts USA supplier on price and lead time. Whichever route you take, ask for a pull-out test certificate on a sample assembly before committing to volume. A single destructive test on your specific tube, insert, adhesive, and surface preparation tells you more than any datasheet, and it gives your quality team a baseline against which production batches can be checked.
Frequently Asked Questions
How strong is a carbon fiber tube insert?
A correctly bonded threaded insert typically sustains 8-15 kN in axial pull-out on a 25 mm tube with a 1.5 mm wall and a four-diameter embedment. Expanding inserts carry less, roughly 2-5 kN, because they grip by friction rather than a bonded area. Press-fit polymer inserts are for light-duty joints only, in the 0.5-2 kN range. The bond quality dominates the result: the same insert with poor surface preparation can lose more than half its capacity, so a pull-out test on the actual assembly is the only reliable number.
Can I glue a threaded insert into a carbon fiber tube myself?
Yes, and it is a common workshop job. Cut and square the tube, abrade the bore with a bottle brush, wipe it with solvent, and mix a two-part structural epoxy. Apply adhesive to both surfaces, insert the fitting with a slight twist to spread the glue, and hold it straight for the full cure time. The two critical details are a thin, uniform adhesive gap of 0.05-0.20 mm and thorough removal of mould release from the tube bore. Without those, the joint can fail at well under half its rated load.
Do carbon fiber tube inserts cause galvanic corrosion?
They can. Carbon fiber is cathodic relative to most metals, so a bare aluminium insert in wet or salt service will drive corrosion of the metal and can eventually loosen the joint. The standard fix is to anodise the aluminium or isolate it from the carbon with a thin glass-fibre or polymer layer. Stainless steel is more resistant than bare aluminium but is still best isolated. For dry indoor frames the risk is low, but any outdoor, marine, or high-humidity application should treat isolation as mandatory.
Conclusion
Carbon fiber tube inserts are small, inexpensive parts that decide whether a composite frame is a reliable structure or a set of loose tubes. Bonded threaded inserts give the highest pull-out strength and the widest fastener range, expanding inserts trade strength for removability, and press-fit polymer inserts suit only light-duty work. The engineering is well understood: prepare the bore, keep the adhesive gap thin and uniform, chamfer edges to avoid peel, and protect against galvanic corrosion whenever the frame sees moisture.
If you are building a carbon fiber frame or replacing a metal structure with a lighter composite one, browse our carbon fiber tube and insert range with pultruded and roll-wrapped tubes in T300, T700, and high-modulus grades plus matching aluminium and stainless inserts, or contact our engineering team for insert selection and a quote for your project.
Part of topic
Related Articles
Interested in Our Products?
Contact our team for competitive pricing and technical specifications.
Get a QuoteRelated Products

Carbon Fiber Plate — 3K Twill T700 3.0mm
Medium-thickness 3.0mm carbon fiber plate offering significantly higher load capacity while maintaining attractive 3K twill finish. Suitable for structural brackets, reinforcement plates, and load-bearing panels.

Carbon Fiber Plate — 3K Twill T700 1.5mm
Thin 1.5mm carbon fiber plate with 3K twill weave surface. Lightweight and stiff, commonly used for covers, panels, drone bodies, and applications requiring a premium aesthetic appearance.

Square Carbon Fiber Tube — 3K Twill T700
Square cross-section carbon fiber tube manufactured with 3K twill weave for torsional strength. Preferred for structural frames, trusses, and support columns where rectangular geometry offers design flexibility.
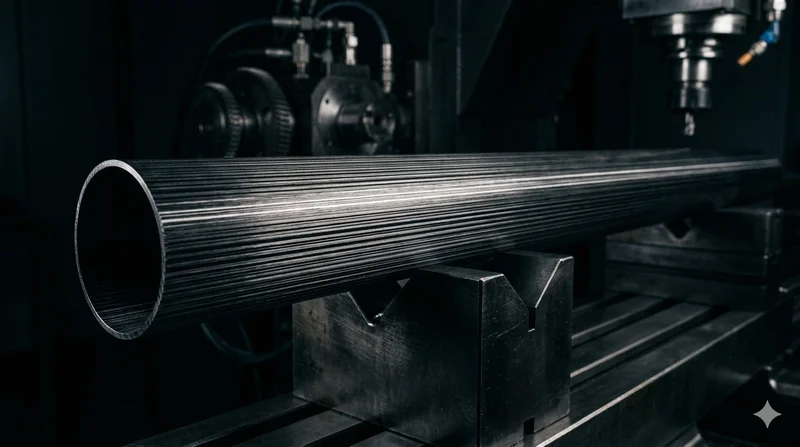
Round Carbon Fiber Tube — UD Unidirectional T700
Unidirectional (UD) round tube with all fibers aligned axially for maximum longitudinal stiffness. Ideal for applications requiring high bending rigidity with minimal weight, such as shafts, struts, and structural reinforcements.
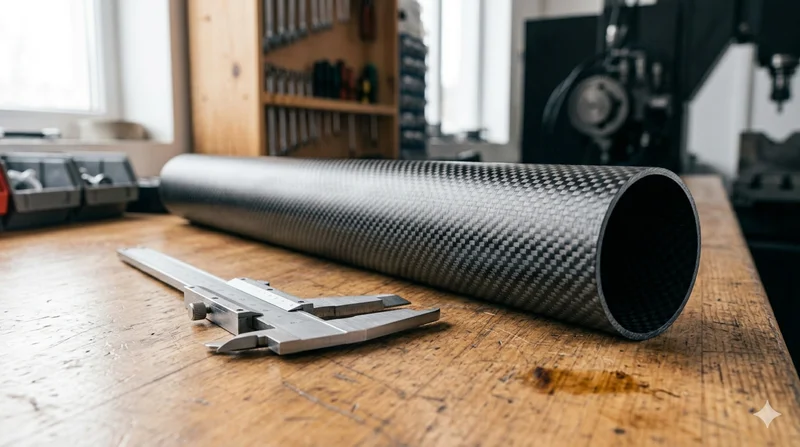
Round Carbon Fiber Tube — 3K Plain Weave T700
Standard round carbon fiber tube manufactured from Toray T700 grade fiber with 3K plain weave. Offers balanced strength and stiffness for general industrial applications including robotics, automation, sports equipment, and aerospace structures.