
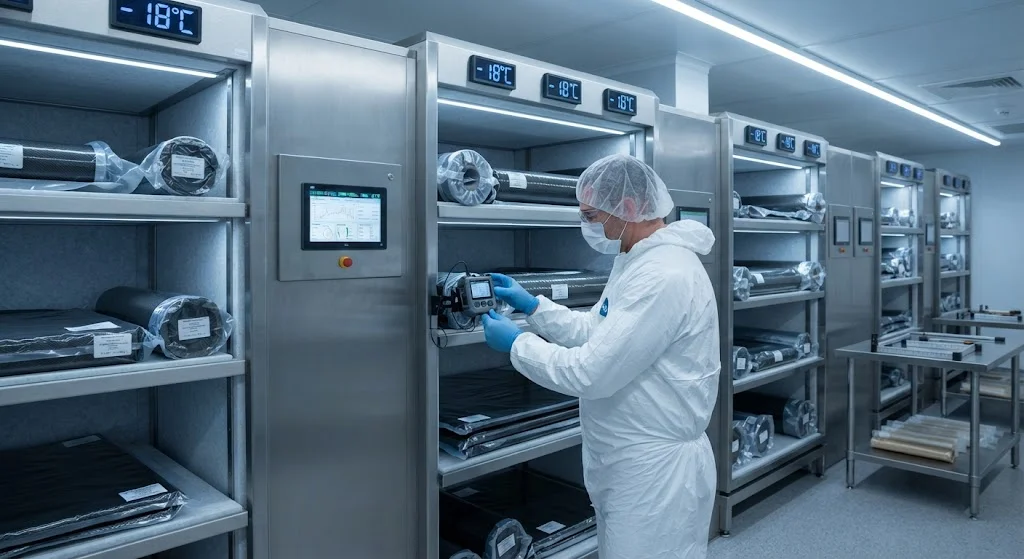
Carbon fiber prepreg materials have limited out-life windows that require strict cold chain management from manufacturing through fabrication. This article examines prepreg storage requirements, out-life degradation mechanisms, cold chain logistics, and quality assurance protocols that ensure consistent composite performance in aerospace, automotive, and industrial applications.
Introduction
Carbon fiber prepreg — pre-impregnated composite material consisting of carbon fiber reinforcement saturated with controlled amounts of uncured thermoset resin (typically epoxy, bismaleimide, or cyanate ester) — represents the highest-performance feedstock in composite manufacturing. The uncured resin system provides excellent handling characteristics, precise resin content control, and repeatable mechanical properties in finished components. However, this uncured state imposes strict time-temperature constraints: prepreg materials have defined "out-life" windows during which they must be stored at controlled temperatures (typically -18°C to -25°C) and fabricated before the resin advances beyond acceptable processing viscosity.
The out-life management challenge is compounded by global supply chains where prepreg may be manufactured in one country, shipped to another for storage, and delivered to fabricators across multiple time zones. Cold chain interruptions, temperature excursions, and documentation gaps can render entire prepreg batches unusable — creating waste costs of $50,000-500,000 per incident and potentially delaying critical aerospace or defense programs. This article examines the science of prepreg aging, cold chain logistics requirements, and quality assurance protocols that enable reliable prepreg management across complex supply networks.
Prepreg Resin Chemistry and Out-Life Fundamentals
Understanding prepreg out-life requires knowledge of the thermoset resin chemistry that governs material aging:
- Resin advancement (B-staging): Uncured epoxy resins undergo slow chemical crosslinking even at refrigerated temperatures, gradually increasing molecular weight and viscosity. This "advancement" is irreversible — once resin viscosity exceeds processing limits (typically 100-500 Pa·s for autoclave cure), prepreg cannot be properly consolidated, resulting in void content >2% and mechanical properties below specification. Rate: resin viscosity doubles approximately every 3 months at -18°C storage.
- Glass transition temperature (Tg) drift: As resin advances, the glass transition temperature of the uncured matrix gradually increases. Tg drift of 5-10°C from initial specification indicates significant advancement and may require requalification of processing parameters. Measurement: Differential Scanning Calorimetry (DSC) per ASTM E2160.
- Tack degradation: Prepreg tack (surface stickiness required for layup consolidation) decreases as resin advances and volatiles evaporate. Insufficient tack creates air entrapment during layup, increasing void content by 1-3% and reducing interlaminar shear strength by 15-25%. Tack testing per ASTM D2979 provides quantitative assessment.
- Volatile accumulation: Uncured prepreg resins emit trace volatile organic compounds (VOCs) that accumulate in sealed packaging. Excessive volatile concentration (typically >500 ppm for aerospace applications) can create porosity during cure. Venting protocols and volatile monitoring are required for long-term storage.
Storage Requirements and Temperature Ranges
Prepreg storage requirements vary by resin system and manufacturer specifications, but follow general categories:
| Resin System | Storage Temperature | Out-Life at -18°C | Out-Life at Room Temp (23°C) | Maximum Temperature Excursion |
|---|---|---|---|---|
| Standard epoxy | -18°C ± 3°C | 12-24 months | 21-30 days | +10°C for 4 hours |
| Fast-cure epoxy | -18°C ± 3°C | 6-12 months | 14-21 days | +5°C for 2 hours |
| Bismaleimide (BMI) | -18°C ± 3°C | 6-12 months | 14-21 days | +5°C for 4 hours |
| Cyanate ester | -25°C ± 5°C | 12-18 months | 21-28 days | +5°C for 2 hours |
| High-temperature epoxy | -25°C ± 5°C | 6-12 months | 14-21 days | +3°C for 2 hours |
Critical storage parameters include:
- Temperature uniformity: Storage facilities must maintain ±3°C uniformity throughout the storage volume. Temperature mapping studies at startup and annually thereafter verify uniformity. Hot spots near compressors or warm spots near walls must be identified and excluded from storage zones.
- Temperature monitoring: Continuous monitoring with calibrated thermocouples (accuracy ±0.5°C) recording at 15-minute intervals minimum. Alarm systems must trigger at ±5°C from setpoint with automated alerts to quality personnel. Data logging must be tamper-evident and retained for 10+ years for aerospace applications.
- Humidity control: While prepreg is sealed in moisture-barrier packaging, storage area humidity should be maintained below 60% RH to prevent condensation during material transfer and reduce corrosion risk for metallic tools and fixtures stored in the same area.
- UV protection: Prepreg must be stored away from direct sunlight or UV sources that can accelerate surface resin advancement. Opaque packaging and controlled lighting (no UV sources) are standard requirements.
Cold Chain Logistics
Maintaining cold chain integrity during prepreg transportation requires coordination between manufacturers, logistics providers, and fabricators:
- Packaging requirements: Prepreg ships in insulated containers with phase-change materials (typically gel packs or dry ice) maintaining -18°C for 48-96 hours depending on transit time. Container qualification testing per ASTM D3103 verifies thermal performance under expected conditions. Inner moisture barrier bags (polyethylene or foil laminate) protect against condensation during temperature transitions.
- Transportation modes: Air freight (24-72 hours) is preferred for time-sensitive aerospace applications, with refrigerated truck transport (3-7 days) for longer routes. Sea freight is generally avoided due to 2-4 week transit times and limited temperature control. Temperature data loggers must accompany each shipment, with data download and review required before material acceptance.
- Customs and regulatory considerations: Prepreg materials classified as hazardous goods (flammable liquids in uncured resin state) require IATA Dangerous Goods Regulations (DGR) compliance for air shipment. Documentation must include Safety Data Sheets (SDS), dangerous goods declarations, and material certifications. Customs delays at border crossings can compromise cold chain integrity — advance documentation and expedited clearance procedures are essential.
- Receiving and inspection: Fabricators must inspect incoming prepreg shipments within 2 hours of delivery, verifying: (1) temperature logger data shows no excursions, (2) packaging integrity (no moisture ingress, no physical damage), (3) material identification matches purchase order specifications. Rejected material must be quarantined and returned to manufacturer for evaluation.
Out-Life Extension and Recovery
When prepreg approaches or exceeds nominal out-life limits, several approaches can extend usable life:
- Re-testing and certification: Prepreg that has been properly stored but exceeds nominal out-life can be re-tested for key properties (viscosity, Tg, tack, volatile content) per ASTM standards. If results meet specification, out-life can be extended by 3-6 months with documented engineering approval. Cost: $5,000-15,000 per batch for complete re-qualification testing.
- Cold storage recovery: Prepreg that experienced minor temperature excursions (within +10°C for <4 hours) may be recoverable if returned to proper storage immediately and tested within 30 days. Recovery eligibility depends on resin system sensitivity and extent of temperature deviation.
- Re-processing: Prepreg with insufficient tack but acceptable resin advancement can sometimes be reprocessed using heated pressure rollers or tack-enhancement treatments. This approach is limited to non-structural applications and requires engineering validation.
Quality Assurance Protocols
Comprehensive quality assurance ensures prepreg consistency throughout the supply chain:
- Incoming material certification: Every prepreg shipment must include Certificate of Conformance (CoC) with: resin content (±2% of specification), volatile content (<1% by weight), gel time (within ±10% of specification), and tack measurement. Manufacturers must provide batch-level traceability linking to raw material certifications.
- Storage condition verification: Quality systems must include daily temperature log review, monthly storage facility audits, and annual temperature mapping studies. Non-conformances must be documented with root cause analysis and corrective actions.
- Out-life tracking: Each prepreg batch must have documented receipt date, storage temperature history, and calculated remaining out-life. Automated inventory management systems track multiple expiry dates (primary out-life, extended out-life after retesting) and generate alerts for material approaching end-of-life.
- Process validation: Fabrication facilities must validate that prepreg processing parameters (layup temperature, autoclave cure cycle) produce acceptable results across the full range of expected out-life. Process windows may require adjustment for material near end-of-life.
Conclusion
Prepreg out-life management and cold chain logistics are critical enablers of high-performance composite manufacturing. The time-temperature sensitivity of uncured thermoset resins demands rigorous storage conditions, transportation controls, and quality assurance protocols throughout the supply chain. As composite applications expand into automotive, wind energy, and industrial sectors with higher-volume production and more diverse supply networks, standardized cold chain management practices and digital tracking technologies will become essential for maintaining material quality and reducing waste.
YongXian CarbonFiber
YongXian manufactures carbon fiber tubes, sheets, and custom composite parts from our Dezhou, China factory. With over 15 years of composite manufacturing experience, we supply carbon fiber components to aerospace, automotive, energy, and industrial customers worldwide.
Contact us for custom carbon fiber solutions.
Part of topic
Related Articles
- Bio-Based Carbon Fiber Precursors: Lignin and Polyethylene for Low-Cost Production
- Large-Tow Carbon Fiber Cost Analysis: 48K vs 60K Price-Performance Comparison
- Carbon Fiber-Resin Interface Bonding: Surface Treatment and Coupling Agent Optimization
- Digital Twin for Carbon Fiber Manufacturing: Real-Time Process Monitoring and Defect Prevention
- Thermoplastic Carbon Fiber Welding for Automotive: Ultrasonic and Induction Welding Process Windows
- Large-Tow Carbon Fiber Wet Spinning: Process Optimization for 48K/60K Production Efficiency